1. The Physics of the 45° Slant Bed #
In production turning environments, machine tool downtime and dimensional drift are almost always caused by two factors: thermal expansion from accumulated hot chips and chatter vibration during heavy cutting.
The Kaida TCK Series (TCK50, TCK52, TCK56) solves these challenges through true 45-degree monolithic slant bed architecture:
A. Natural Gravity Chip Evacuation
On a conventional flat bed lathe, hot metal chips fall directly onto the bedways and cross slide, requiring manual raking or localized wash-down pumps. Over long shifts, hot chips transfer thermal energy into the bed castings, causing Z-axis thermal drift. On the Kaida TCK 45° slant bed, chips fall directly into the low-mounted automatic chain chip conveyor without contacting the guide rails or ball screws, maintaining consistent part diameters from first piece to last.
B. Direct Compression Force Loading
During turning, the cutting tool exerts force down and back toward the spindle center. On a 45° slant bed, this resultant cutting force vector points directly perpendicular into the heavy triangular Meehanite cast base. Cast iron exhibits approximately 4 to 5 times higher compressive strength than shear strength, eliminating carriage lift and tool chatter.
2. High-Speed Production Features of the Kaida TCK Line #
- 0.2-Second Servo Turret Indexing: The 8-station hydraulic or 12-station servo turret uses a three-piece curvic coupling clamp, ensuring sub-micron tool positioning repeatability.
- 24 m/min Rapid Feed Rates: Precision roller linear guideways minimize friction, allowing rapid tool approach and retract cycles.
- Programmable Hydraulic Tailstock: Automatic quill advance and retract coordinated with the CNC cycle simplifies shaft machining.
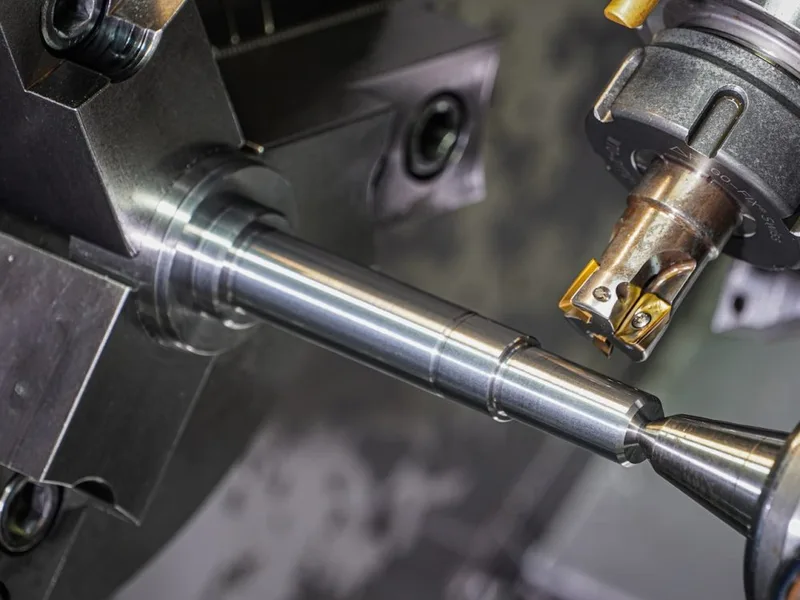
- Live Tooling & C-Axis (BMT Option): Perform cross-drilling, keyway milling, and tapping in a single clamping setup, eliminating secondary milling operations.
3. TCK Series Model Breakdown #
- TCK50: Max swing Ø500mm, Ø360mm turning dia, 8" chuck, 4,000 RPM spindle. Ideal for high-speed automotive pins, hydraulic connectors, and precision bushings.
- TCK52: Heavy 10" chuck with A2-8 spindle and Ø86mm bore. Engineered for pump impellers, gear blanks, and forged flange machining.
- TCK56: Large bore heavy turning center with up to Ø105mm spindle through-hole. Built for heavy drill collars, API couplings, and railway components.
Request a cycle time estimate for your turned parts: xiuc32860@gmail.com.